Why nylon is the material that punishes the careless moulder
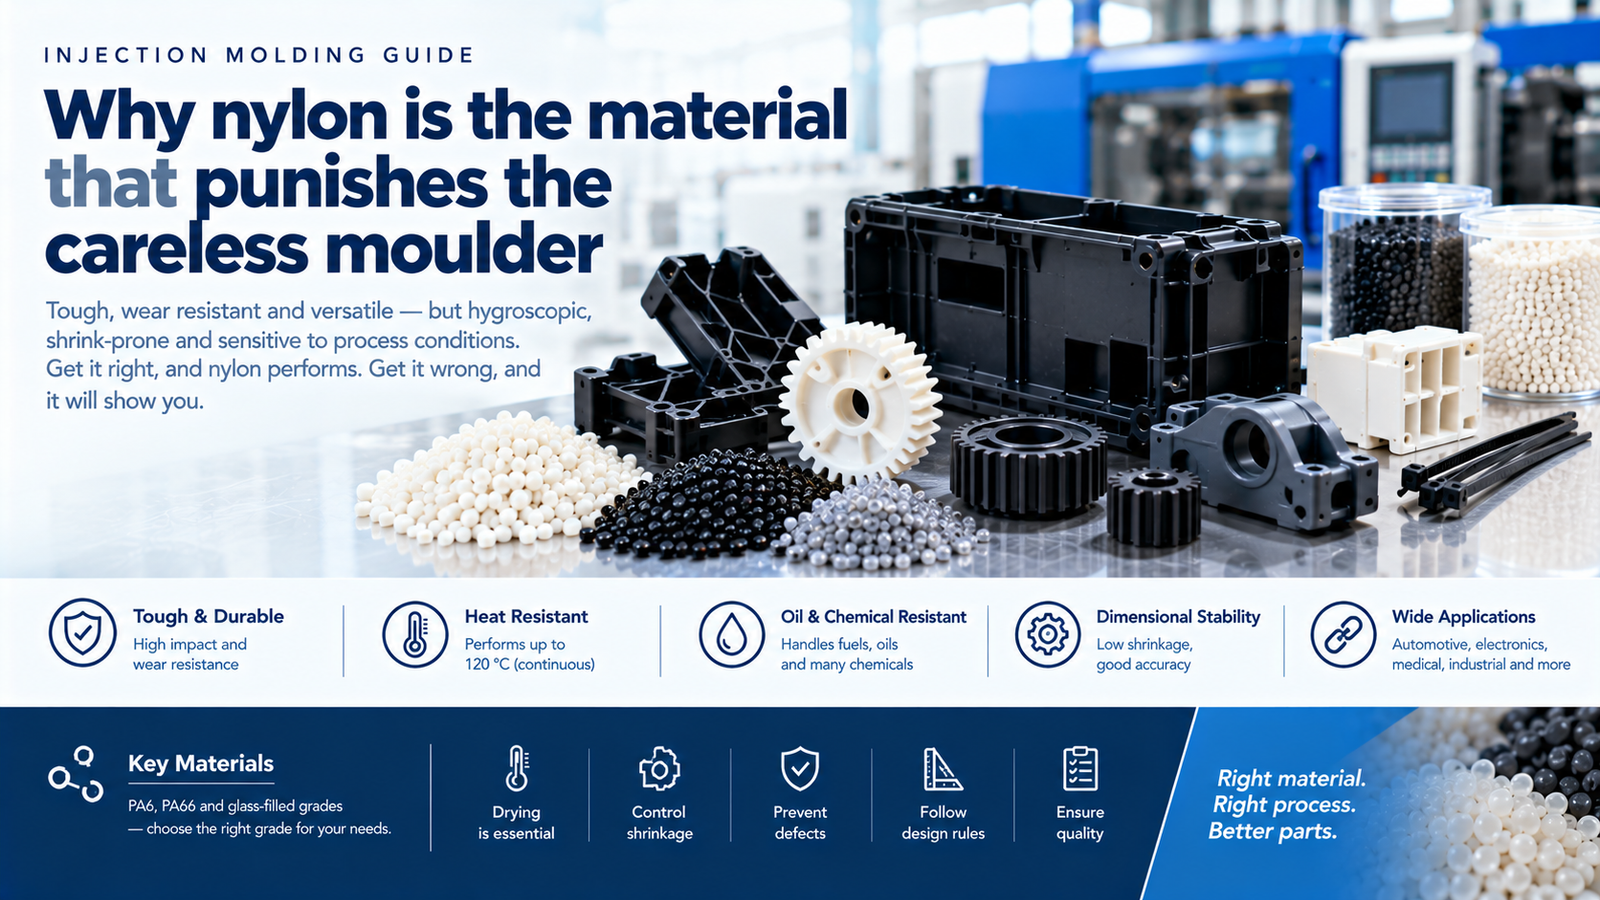
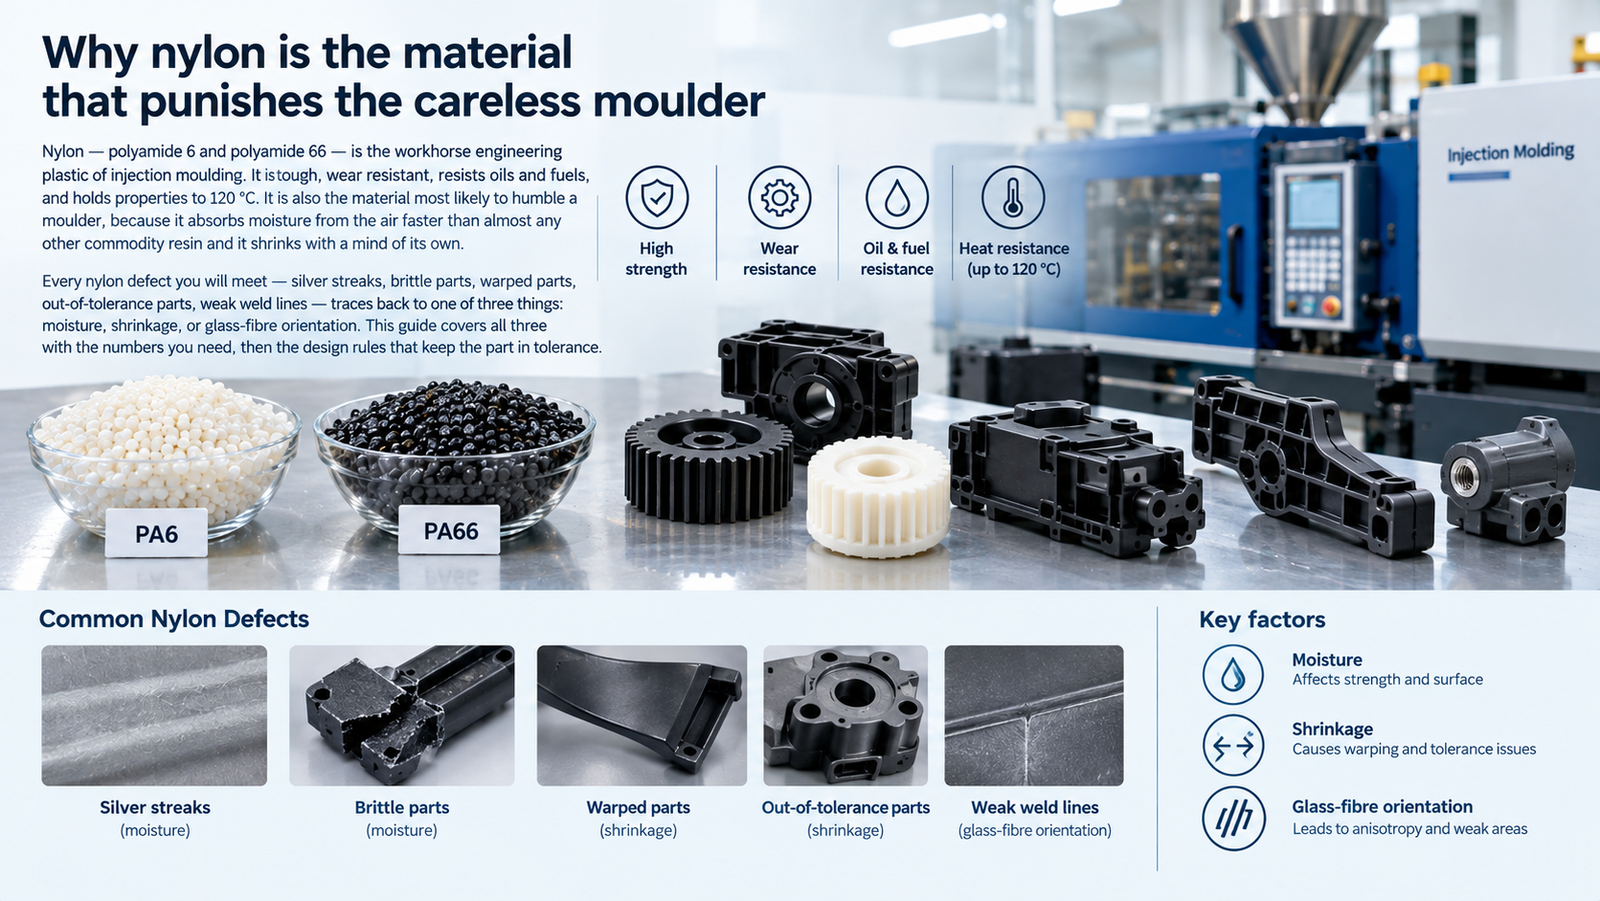
Nylon — polyamide 6 and polyamide 66 — is the workhorse engineering plastic of injection moulding. It is tough, wear resistant, resists oils and fuels, and holds properties to 120 °C. It is also the material most likely to humble a moulder, because it absorbs moisture from the air faster than almost any other commodity resin and it shrinks with a mind of its own.
Every nylon defect you will meet — silver streaks, brittle parts, warped parts, out-of-tolerance parts, weak weld lines — traces back to one of three things: moisture, shrinkage, or glass-fibre orientation. This guide covers all three with the numbers you need, then the design rules that keep the part in tolerance.
Nylon injection molding is the workhorse of engineering plastics. Polyamide 6 and polyamide 66 are tough, wear resistant, resist oils and fuels, and hold properties to 120 °C.
PA6 versus PA66: choose on temperature, not habit
Both are polyamides, but they are not interchangeable. PA66 has a higher melting point and better heat resistance; PA6 has better flow, better surface finish and slightly better impact at low temperature.
| Property | PA6 | PA66 |
|---|---|---|
| Melting point (°C) | 220 | 255 – 265 |
| Typical melt temperature (°C) | 230 – 260 | 270 – 300 |
| Mould temperature (°C) | 60 – 90 | 70 – 110 |
| Continuous service temperature (°C) | 90 – 105 | 100 – 120 |
| Water absorption, 24 h (%) | 1.3 – 1.9 | 1.0 – 1.5 |
| Water absorption, saturated (%) | 9 – 10 | 8 – 8.5 |
| Unfilled mould shrinkage (%) | 0.6 – 1.4 | 0.8 – 1.5 |
| Notched impact, dry (kJ/m²) | 4 – 6 | 3 – 5 |
| Notched impact, conditioned (kJ/m²) | 15 – 25 | 10 – 20 |
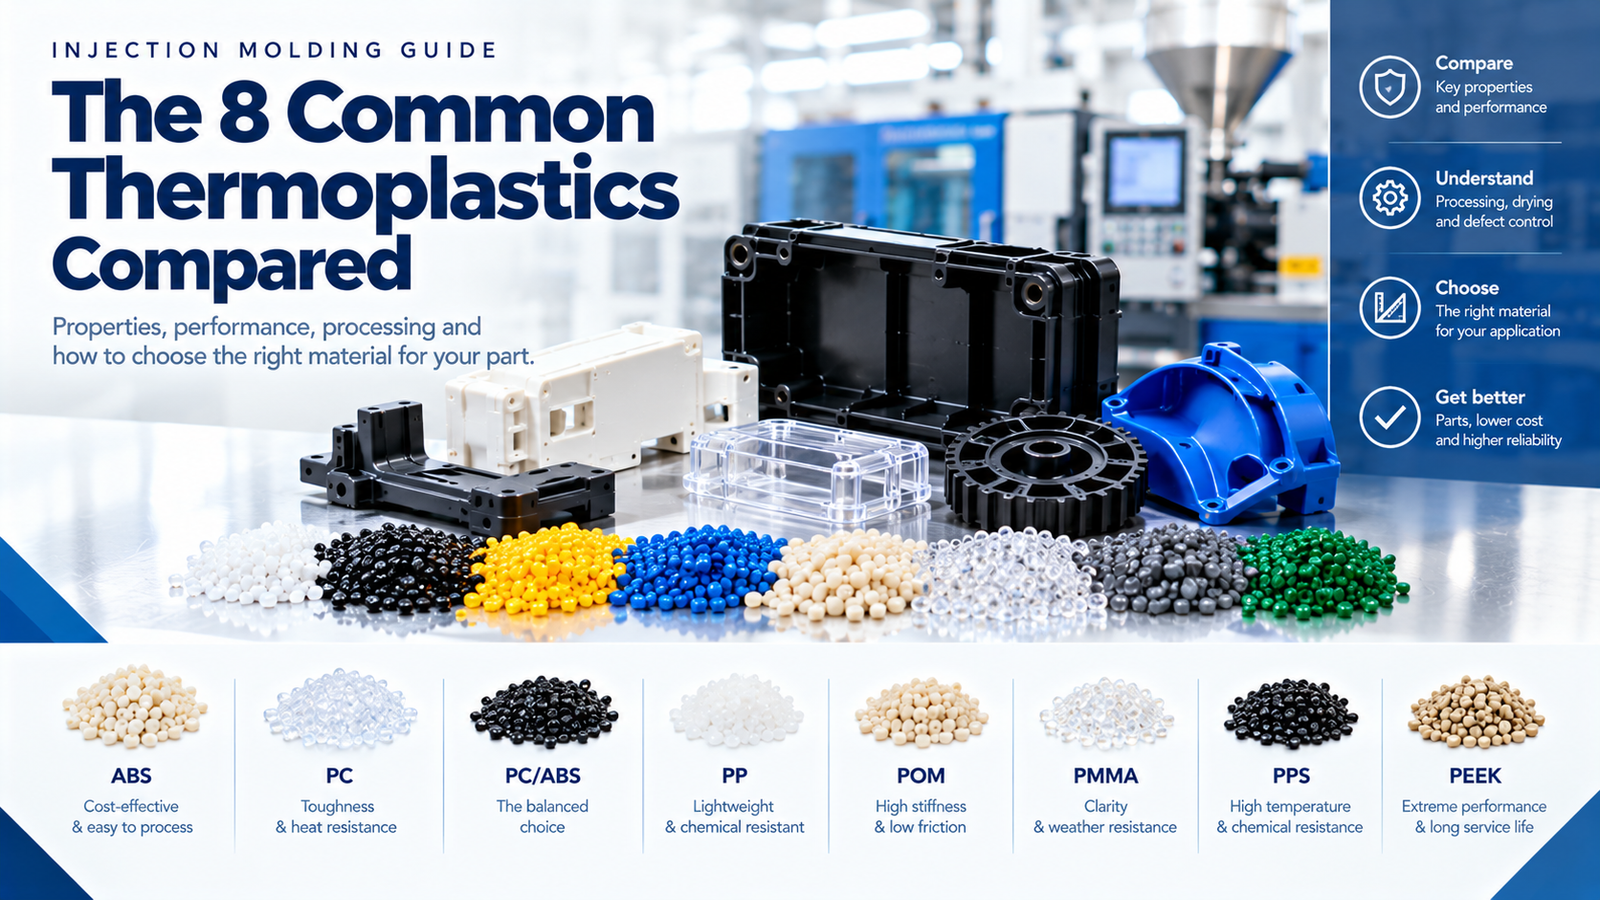
The practical rule: if the part sees above 100 °C continuously, or needs stiffness at temperature, use PA66. If it needs flow into thin walls, a cosmetic surface, or maximum toughness after conditioning, PA6 is often the better choice. For side-by-side comparisons, see how PA66 compares with POM and PA66 against PBT and PPS.
Drying is not a step you can skip
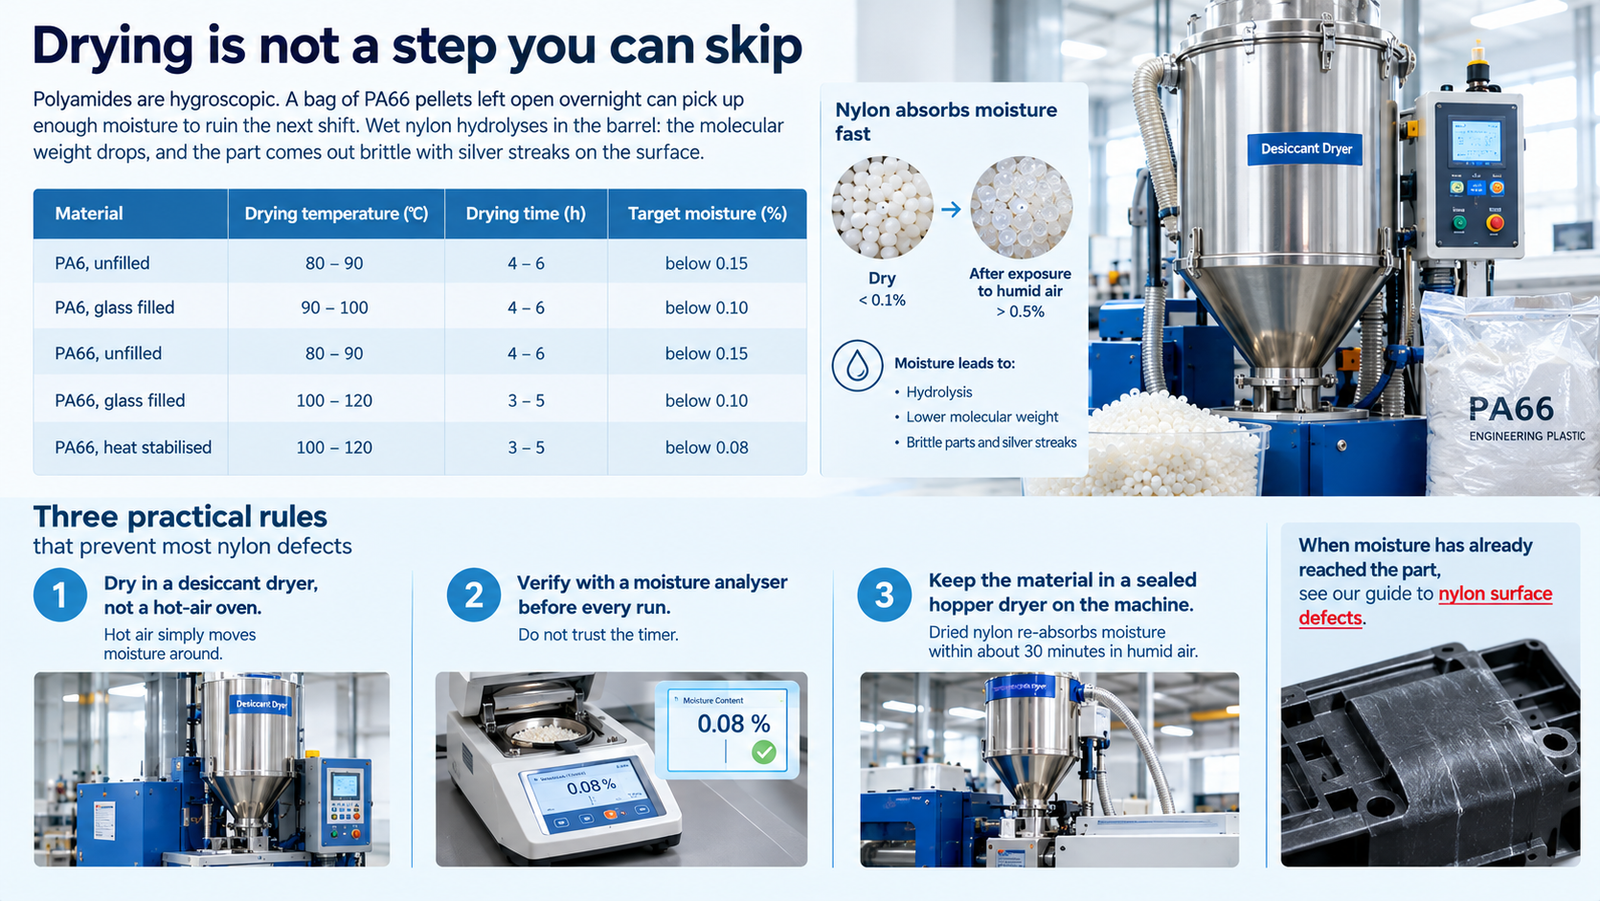
Polyamides are hygroscopic. A bag of PA66 pellets left open overnight can pick up enough moisture to ruin the next shift. Wet nylon hydrolyses in the barrel: the molecular weight drops, and the part comes out brittle with silver streaks on the surface.
| Material | Drying temperature (°C) | Drying time (h) | Target moisture (%) |
|---|---|---|---|
| PA6, unfilled | 80 – 90 | 4 – 6 | below 0.15 |
| PA6, glass filled | 90 – 100 | 4 – 6 | below 0.10 |
| PA66, unfilled | 80 – 90 | 4 – 6 | below 0.15 |
| PA66, glass filled | 100 – 120 | 3 – 5 | below 0.10 |
| PA66, heat stabilised | 100 – 120 | 3 – 5 | below 0.08 |
Three practical rules that prevent most nylon defects:
First, dry in a desiccant dryer, not a hot-air oven — hot air simply moves moisture around. Second, verify with a moisture analyser before every run; do not trust the timer. Third, keep the material in a sealed hopper dryer on the machine, because dried nylon re-absorbs moisture within about 30 minutes in humid air. When moisture has already reached the part, see our guide to nylon surface defects.
Shrinkage and warpage: the numbers
Unfilled nylon shrinks 0.8 – 1.5% (PA66) or 0.6 – 1.4% (PA6) and the shrinkage continues after ejection as the part crystallises and absorbs moisture. That post-mould growth is the reason nylon parts measured at the press can be out of tolerance 24 hours later.
| Grade | Shrinkage, flow direction (%) | Shrinkage, cross flow (%) |
|---|---|---|
| PA66 unfilled | 0.8 – 1.5 | 1.0 – 1.8 |
| PA66 GF30 | 0.2 – 0.5 | 0.8 – 1.2 |
| PA66 GF50 | 0.1 – 0.3 | 0.6 – 1.0 |
| PA6 unfilled | 0.6 – 1.4 | 0.9 – 1.7 |
| PA6 GF30 | 0.3 – 0.6 | 0.9 – 1.4 |
Glass fibre reduces shrinkage along the flow direction far more than across it, and that difference is what warps glass-filled nylon parts: the material wants to shrink differently in two directions. The design answers are uniform wall thickness, symmetrical glass distribution, generous radii, and gate positions that let the fibre orientation balance out. For the full correction method, see reducing warpage in PA66 parts.
Glass-filled grades change the rules
Adding 30% glass fibre roughly doubles tensile strength and triples stiffness, raises heat deflection temperature by 40 – 60 °C, and cuts shrinkage — but it also brings abrasion, anisotropy and a dull surface.
| Property | PA66 unfilled | PA66 GF30 | PA66 GF50 |
|---|---|---|---|
| Tensile strength (MPa) | 80 – 85 | 150 – 185 | 200 – 230 |
| Tensile modulus (MPa) | 3,000 | 9,000 – 10,000 | 15,000 – 17,000 |
| HDT at 1.8 MPa (°C) | 70 – 90 | 240 – 250 | 250 – 255 |
| Density (g/cm³) | 1.14 | 1.36 | 1.56 |
Glass-filled nylon needs hardened tool steel, larger gates, higher melt temperature, higher mould temperature and more injection pressure. It also wears out screws and check rings, so barrel life is a real cost factor. The processing differences are compared in glass-filled versus pure nylon.
The processing window
| Parameter | PA66 unfilled | PA66 glass filled | PA6 unfilled |
|---|---|---|---|
| Melt temperature (°C) | 270 – 290 | 280 – 300 | 230 – 260 |
| Mould temperature (°C) | 70 – 90 | 90 – 110 | 60 – 90 |
| Injection pressure (bar) | 700 – 1,200 | 900 – 1,500 | 600 – 1,100 |
| Hold pressure (% of injection) | 40 – 60 | 50 – 70 | 40 – 60 |
| Back pressure (bar) | 20 – 50 | 30 – 60 | 20 – 50 |
| Screw speed (rpm) | 60 – 100 | 50 – 80 | 70 – 110 |
Higher mould temperature raises crystallinity, which improves dimensional stability, surface finish and fatigue life — but extends cycle time. For tolerance-critical parts, the extra seconds are usually worth it.
The defects you will actually meet
Silver streaks and bubbles. Moisture. Nothing else. Dry the material properly and they disappear.
Brittle parts. Also moisture, or thermal degradation from sitting too long at temperature. Check the residence time against the barrel capacity.
Warpage. Uneven wall thickness, asymmetric glass orientation, or uneven cooling. Fix the part design before you touch the process.
Short shots on glass-filled grades. Higher viscosity plus small gates. Increase gate size, raise melt temperature, increase injection speed.
Flash at the parting line. Excessive packing pressure combined with low clamp force relative to the projected area. Nylon's low viscosity finds every gap.
Weak weld lines. Weld lines in nylon lose 40 – 60% of their strength, and more in glass-filled grades because the fibre does not cross the weld. Move the gate, add a overflow well, or raise melt and mould temperature to improve knitting.
Design rules that save the tool
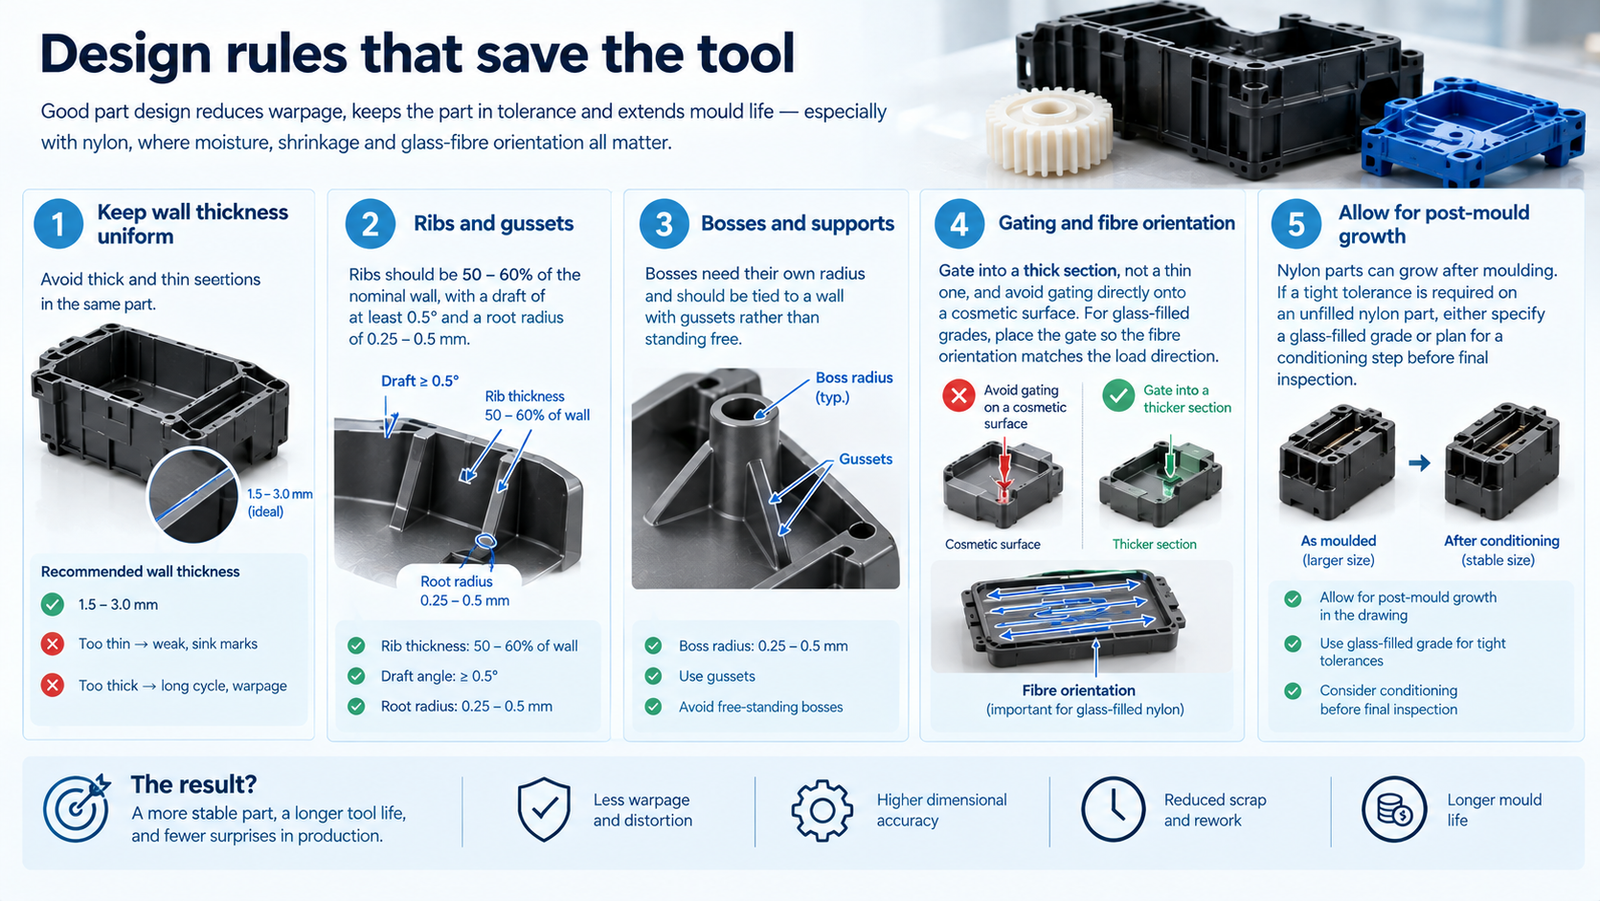
Keep wall thickness uniform, ideally 1.5 – 3.0 mm. Ribs should be 50 – 60% of the nominal wall, with a draft of at least 0.5° and a root radius of 0.25 – 0.5 mm. Bosses need their own radius and should be tied to a wall with gussets rather than standing free.
Gate into a thick section, not a thin one, and avoid gating directly onto a cosmetic surface — nylon gate marks are difficult to polish out. For glass-filled grades, place the gate so the fibre orientation matches the load direction.
Allow for post-mould growth. If the drawing calls for a tight tolerance on an unfilled nylon part, either specify a glass-filled grade or plan for a conditioning step before final inspection.
Where nylon earns its place
Nylon dominates where toughness, wear resistance and oil resistance matter together: bushings, gears, cable ties, clips, automotive under-hood brackets, engine covers, battery cases, gaskets, agricultural machinery components, power tool housings and conveyor parts.
Glass-filled PA66 is the standard for structural brackets and battery enclosures; unfilled PA6 suits cosmetic covers and parts that need impact after conditioning. See how GF-PA66 battery cases run in volume, how nylon compares with POM for gears, or return to our injection moulding materials overview.
Material data in this guide follows the test methods published by ASTM International and ISO, with typical values cross-checked against MatWeb and Engineering Toolbox. Processing practice follows Plastics Technology guidance and PLASTICS industry standards, with material characterisation maintained through SPE and NIST reference data. For the polymer chemistry, see nylon.
Does nylon always need drying before moulding?
Yes. Both PA6 and PA66 absorb moisture from the air and hydrolyse in the barrel if they are wet. Dry to below 0.15% moisture (0.10% for glass-filled grades) and keep the material in a sealed hopper dryer during running.
Should I choose PA6 or PA66?
Choose PA66 when the part sees continuous temperatures above 100 °C or needs stiffness at temperature. Choose PA6 when you need better flow into thin walls, a better cosmetic surface, or maximum toughness after moisture conditioning.
Why do my glass-filled nylon parts warp?
Because glass fibre reduces shrinkage much more along the flow direction than across it. Uneven fibre orientation, uneven wall thickness or uneven cooling then pulls the part out of shape. Fix it with balanced gating, uniform walls and symmetrical cooling.
How much do weld lines weaken a nylon part?
Typically 40 – 60% of the base material's tensile strength at the weld, and more in glass-filled grades because the fibre does not cross the weld line. Reposition the gate, add an overflow well, or raise melt and mould temperature to improve knitting.
Can nylon parts hold tight tolerances?
Yes, but only with the right grade and process. Glass-filled PA66 with a hot mould and uniform walls can hold ±0.05 mm on critical dimensions. Unfilled nylon continues to grow after moulding as it absorbs moisture, so allow for conditioning before final inspection.
What is the maximum service temperature for PA66?
Around 100 – 120 °C continuous for unfilled grades, and up to 240 – 250 °C heat deflection temperature for glass-filled grades under load. Always design 20 – 30 °C below the data sheet value and check heat deflection under the real load.
Conclusion
Nylon rewards discipline. Dry it properly, respect its shrinkage, balance the glass orientation, and it will deliver tough, accurate, oil-resistant parts year after year. Skip any of those three and it will produce brittle, warped or out-of-tolerance parts no matter how good the tool is.
At Rui Cheng we mould PA6 and PA66, unfilled and glass filled from 15% to 50%, on 80 to 1,400 tonne machines, with in-house tooling, ±0.02 mm tolerance capability and ISO 9001 / IATF 16949 processes. Send us your drawing, the service temperature, chemical exposure and annual volume, and we will come back with a grade recommendation, a drying and process window, and an indicative part cost.
For more detail on specific nylon topics, see our guides on warpage control, glass-filled versus unfilled processing, surface defects, and material selection against POM, PBT and PPS.