PEEK sits at the top of the engineering plastics pyramid. It holds its properties at temperatures that destroy nylon and PBT, resists nearly every chemical a plant will throw at it, wears against steel better than most filled materials, survives steam and hydrolysis indefinitely, and is available in grades qualified for implantation in the human body. It also costs ten to twenty times more than polypropylene, melts at 343 °C, and demands a melt temperature of 380 to 400 °C with a mould running above 175 °C — which puts it in a completely different processing regime from every commodity plastic.
This guide covers PEEK injection moulding as a production process: grades, the processing window, tooling requirements, shrinkage, drying, defect control, cost structure, applications and quality documentation.
What Makes PEEK Different
| Property | PEEK behaviour | What it means in practice |
|---|---|---|
| Structure | Semi-crystalline (about 30 to 35 percent crystallinity) | Excellent solvent resistance and fatigue performance above the glass transition |
| Melting point | Approximately 343 °C | Melt temperature 380 to 400 °C — far above any standard machine setup |
| Glass transition | Approximately 143 °C | Properties are retained well above the Tg because of the crystalline phase |
| Continuous service temperature | Around 250 °C | The highest of any common mouldable thermoplastic |
| Density | About 1.30 g per cubic centimetre | Readily filled with glass or carbon fibre to raise stiffness further |
| Chemical resistance | Outstanding, including against many solvents | The standard material for chemical, oil and gas and semiconductor service |
| Hydrolysis resistance | Excellent | Survives repeated steam and hot water sterilisation where other polymers fail |
| Wear | Good unfilled, excellent in bearing grades | Direct replacements for metal bushings in dry-running applications |
| Creep | Low, and retained at temperature | Load-bearing parts keep their dimensions in hot service |
| Burning behaviour | Inherently flame retardant with low smoke and toxicity | Preferred in aerospace, rail and mass transit interiors |
| Cost | Ten to twenty times commodity plastics | Justified only where service conditions rule everything else out |
| Processing | 380 to 400 °C melt, mould above 175 °C | Requires specialised tooling, heating equipment and experienced process control |
The theme is simple: PEEK is specified when the service conditions exclude every cheaper option. Heat is the condition that decides most PEEK projects, and our note on whether PEEK parts withstand long-term heat exposure works through what the material actually does at temperature. That means the engineering effort per part is usually higher, and the material cost is almost never the deciding factor in the design.
PEEK Grades and What Each One Is For
| Grade | What it adds | Typical use |
|---|---|---|
| Unfilled | Balanced stiffness, toughness and chemical resistance | Chemical components, seals, insulators, general high-temperature parts |
| Glass filled 30 percent | Higher stiffness and better dimensional stability at temperature | Structural parts, housings, pump components |
| Carbon filled 30 percent | Highest specific stiffness, low creep, good thermal conductivity | Aerospace structures, precision machine parts |
| Carbon and PTFE bearing grade | Lowest friction with high load capacity | Bearings, bushings, thrust washers, seals |
| Carbon, graphite and PTFE | Maximum wear performance and thermal conductivity | High-pressure, high-velocity bearing applications |
| Medical and implant grades | Biocompatibility documentation and batch traceability | Surgical instruments, dental components and implantable devices |
| Food and drink contact grades | Compliance for repeated contact and sterilisation | Food processing equipment, dairy and beverage parts |
| Unfilled natural and coloured | Neutral base for machined and moulded parts | Prototypes, general industrial parts |
Grade choice follows the load case and the service environment, not the polymer name. A bearing part specified in unfilled PEEK instead of a carbon and PTFE grade will fail early, and a structural part specified in a bearing grade wastes stiffness and money.
Processing PEEK: A Different Regime
| Parameter | Typical range | Note |
|---|---|---|
| Melt temperature | 380 to 400 °C | Verified with an air shot, not read from the controller |
| Mould temperature | 175 to 200 °C | Oil-heated tooling is normal — mould temperature drives crystallinity and performance |
| Drying | 150 to 160 °C for 3 to 4 hours | Essential; PEEK is dried before processing as standard practice |
| Residence time | Keep as short as practical | PEEK is more thermally stable than POM or PBT but not immune to long dwell times |
| Screw and barrel | Corrosion-resistant, high-temperature rated | The machine must be rated for 400 °C with the correct screw metallurgy |
| Tool steel | Hardened, corrosion-resistant grades | High mould temperature stresses tooling; thermal expansion must be designed in |
| Tool heating | Oil circulation, not water | Water-based temperature control cannot reach 175 to 200 °C reliably |
| Gates | Generous, with generous radii | Small gates shear the melt and create weak points in a part nobody wants to scrap |
| Venting | Correctly sized but adequate | Trapped gas at 400 °C degrades the material quickly |
| Purging | Dedicated high-temperature purge compound | Never leave PEEK sitting hot in the barrel |
| Regrind | Limited and re-dried | Degraded PEEK loses the very properties the part was specified for |
The mould temperature is the parameter that decides whether a PEEK part is good or merely moulded. Running a PEEK tool at 120 °C instead of 180 °C produces a part with lower crystallinity, poorer chemical resistance, worse dimensional stability and a lower service temperature — all of the reasons the material was chosen in the first place.
Because the tool must run hot, an ordinary water-cooled mould will not do. PEEK tooling is built around oil circulation units, thermal expansion allowances that account for a tool growing several tenths of a millimetre between cold and hot, and hardened, corrosion-resistant steel. This is one of the reasons PEEK tooling costs more than a comparable polypropylene tool, and why the process should be planned with a moulder who runs it routinely. Our note on verifying a supplier's expertise in high-temperature and chemically resistant materials covers the questions worth asking before a project starts.
Shrinkage and Dimensional Control
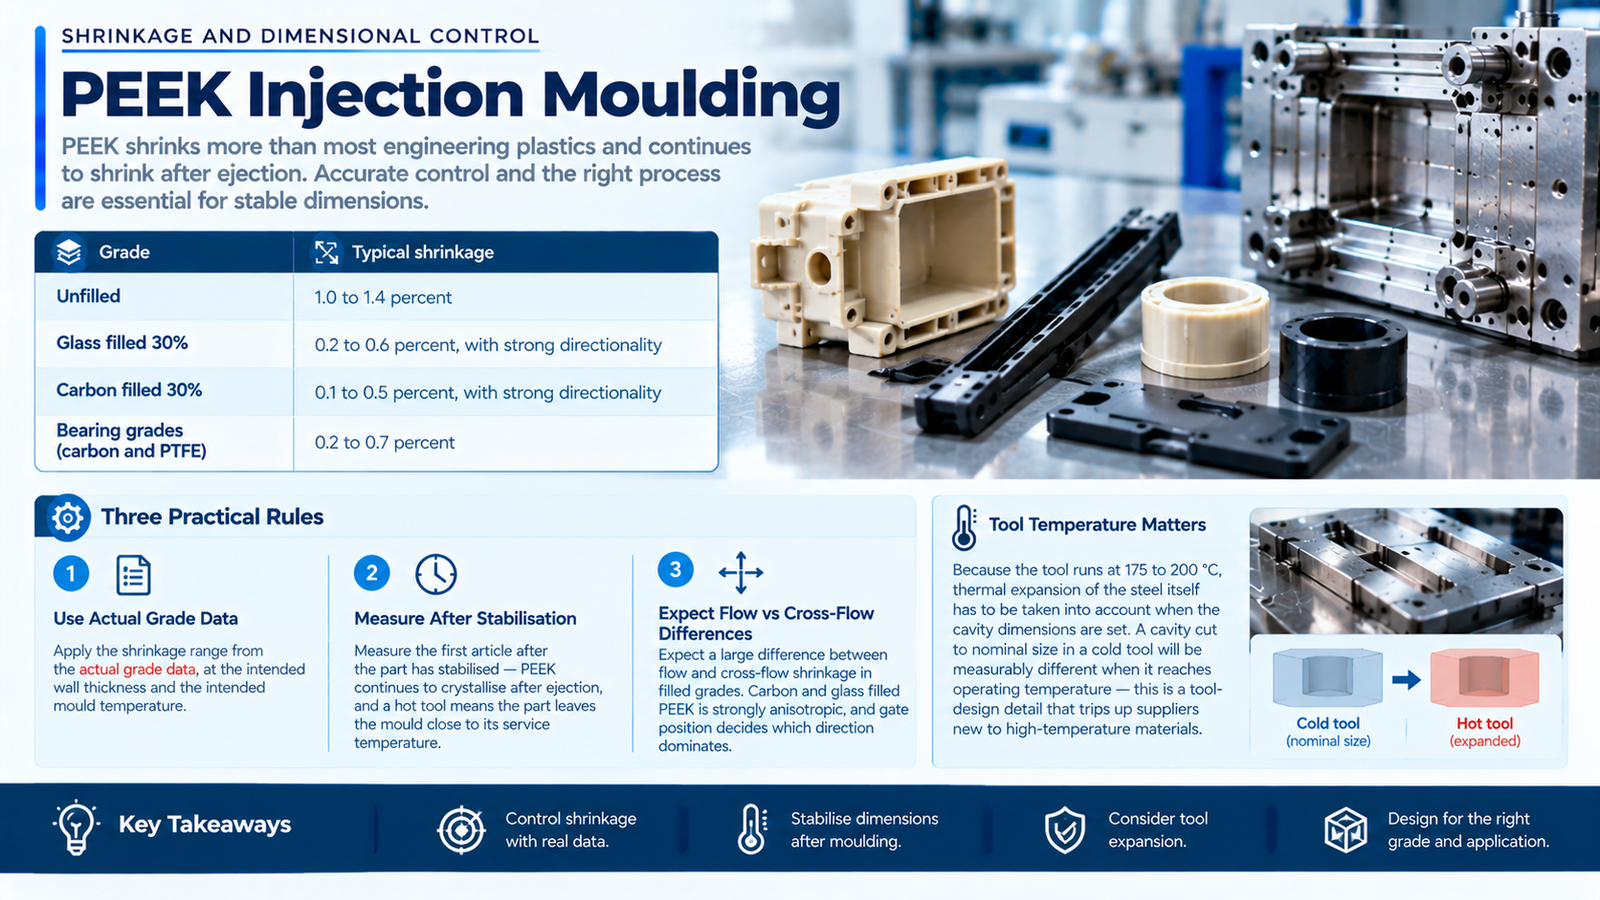
| Grade | Typical shrinkage |
|---|---|
| Unfilled | 1.0 to 1.4 percent |
| Glass filled 30 percent | 0.2 to 0.6 percent, with strong directionality |
| Carbon filled 30 percent | 0.1 to 0.5 percent, with strong directionality |
| Bearing grades (carbon and PTFE) | 0.2 to 0.7 percent |
Three practical rules apply:
- Apply the shrinkage range from the actual grade data, at the intended wall thickness and the intended mould temperature.
- Measure the first article after the part has stabilised — PEEK continues to crystallise after ejection, and a hot tool means the part leaves the mould close to its service temperature.
- Expect a large difference between flow and cross-flow shrinkage in filled grades. Carbon and glass filled PEEK is strongly anisotropic, and gate position decides which direction dominates.
Because the tool runs at 175 to 200 °C, thermal expansion of the steel itself has to be taken into account when the cavity dimensions are set. A cavity cut to nominal size in a cold tool will be measurably different when it reaches operating temperature — this is a tool-design detail that trips up suppliers new to high-temperature materials.
Drying PEEK
PEEK is dried before processing as standard practice rather than as an exception. The recommendation is typically 150 to 160 °C for 3 to 4 hours in a desiccant dryer, with the material kept dry up to the feed throat.
| Situation | Action |
|---|---|
| Sealed, freshly delivered material | Dry per the supplier's recommendation before use |
| Opened bags or material stored in a humid area | Always dry |
| Regrind | Always dry, and check for degradation |
| Medical and implant grades | Follow the material certificate and the qualified process exactly |
| Surface defects on the part | Check drying before changing anything else |
Moisture in PEEK shows up as splay, silver streaks and reduced mechanical performance — the same signatures as other polymers, but far more expensive to discover after a run of parts.
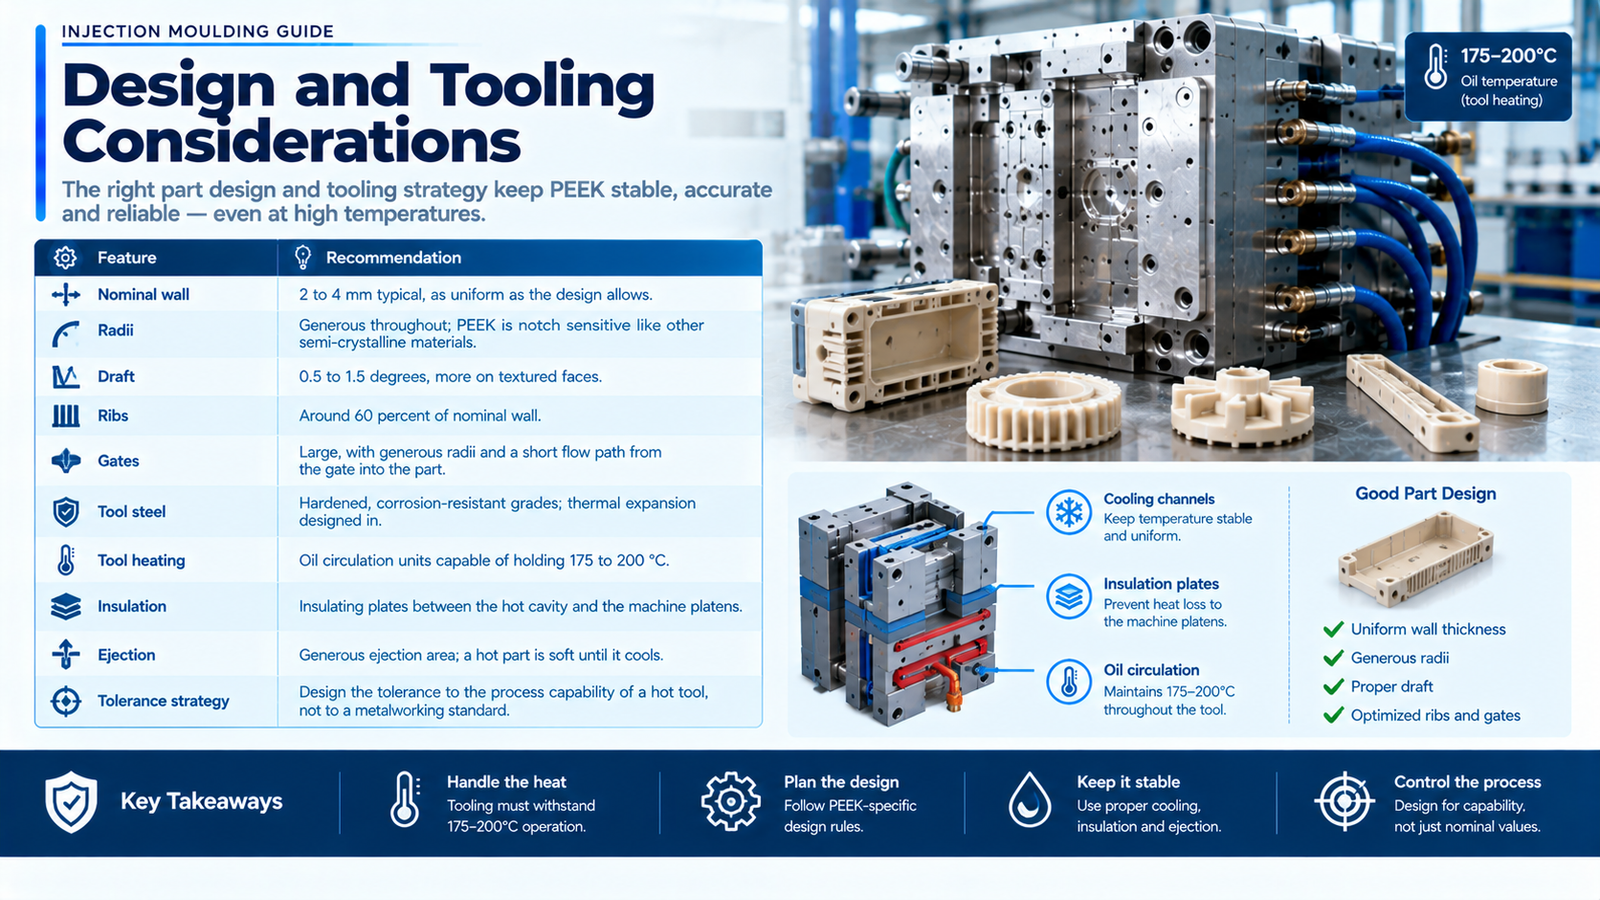
Design and Tooling Considerations
| Feature | Recommendation |
|---|---|
| Nominal wall | 2 to 4 mm typical, as uniform as the design allows |
| Radii | Generous throughout; PEEK is notch sensitive like other semi-crystalline materials |
| Draft | 0.5 to 1.5 degrees, more on textured faces |
| Ribs | Around 60 percent of nominal wall |
| Gates | Large, with generous radii and a short flow path from the gate into the part |
| Tool steel | Hardened, corrosion-resistant grades; thermal expansion designed in |
| Tool heating | Oil circulation units capable of holding 175 to 200 °C |
| Insulation | Insulating plates between the hot cavity and the machine platens |
| Ejection | Generous ejection area; a hot part is soft until it cools |
| Tolerance strategy | Design the tolerance to the process capability of a hot tool, not to a metalworking standard |
PEEK part design rewards the same discipline as any semi-crystalline material, with one addition: everything about the tool has to survive being hot all day. Cooling channels, ejector systems, seals and sensors are all affected, and an under-designed tool will leak oil or seize long before it wears out.
Common Defects and Troubleshooting
| Defect | Likely cause | Fix |
|---|---|---|
| Black specks and discoloration | Degradation from overheating or long residence time | Reduce melt temperature and dwell, purge thoroughly, inspect the screw and non-return valve |
| Short shots | Cold melt, insufficient pressure, undersized gate | Raise melt and mould temperature, increase injection speed, enlarge the gate |
| Weak weld lines | Low mould temperature, poor venting | Raise mould temperature, add venting at the weld location |
| Warpage | Uneven crystallinity from unbalanced tool temperature | Balance the oil circuits, review gate position and hold profile |
| Surface splay or silver streaks | Moisture, or degradation | Dry the material to specification, verify melt temperature |
| Voids in thick sections | Insufficient packing in a thick wall | Reduce wall thickness, adjust hold profile and gate position |
| Sticking and ejection marks | Hot, soft part or excessive packing | Review ejection area, mould temperature and hold pressure |
| Part fails in service | Wrong grade for the load case, or reduced crystallinity | Confirm the grade, verify mould temperature and crystallinity |
Most PEEK problems come down to two root causes: heat history and mould temperature. Both are measurable, and both should be recorded on the process sheet for every job.
Cost: Why PEEK Parts Cost What They Cost
Buyers are often surprised by PEEK part pricing, so it is worth breaking the cost down.
| Cost driver | Practical effect |
|---|---|
| Material price | Ten to twenty times commodity plastics; a single part can cost more in resin than a PP part costs complete |
| Moisture control | Drying, sealed handling and rejected material all add cost |
| Machine capability | Only high-temperature machines with corrosion-resistant screws and barrels can run it |
| Tooling | Hot-oil tool heating, hardened steels, insulation and thermal expansion design |
| Energy | Holding a barrel at 400 °C and a tool at 180 °C is expensive, all day |
| Yield | Process windows are narrower, so scrap rates are higher than on commodity jobs |
| Documentation | Medical, aerospace and semiconductor customers require traceability and certificates |
For development work before tooling is committed, our note on whether rapid prototyping can handle PEEK and other specialty plastics covers what is practical. The honest framing for a PEEK quotation is that the material and the process are both premium, and the part is worth it only where the service environment demands it. When a PEEK part is genuinely over-specified, moving to PPS, PEI or a filled PBT can cut cost substantially without losing the required performance — a comparison worth making at the design stage.
Where PEEK Wins
- Aerospace — structural brackets, fluid fittings, bushings and interior components, where low smoke and toxicity matter
- Medical and dental — surgical instruments, dental components and implantable devices in the appropriate grades
- Semiconductor — wafer handling components that must resist plasma and chemicals without contaminating the process
- Oil and gas — seals, back-up rings and downhole components exposed to hot hydrocarbons and sour service
- Chemical processing — pump components, valve parts, seals and wear rings
- Automotive and EV — high-voltage insulation, bearing cages and transmission components in hot or dry-running locations
- Bearing and wear applications — where a metal bushing needs replacing with something that runs dry. The parameters worth checking before specifying a bearing part are set out in our guide to wear-resistant PEEK parts for high-end bearings.
- Drone and lightweight structures — where specific stiffness and thermal stability both matter
Where a part must combine light weight with thermal stability, the design criteria are specific enough that they are worth stating explicitly before material selection — our note on the metrics for lightweight PEEK parts in drones is one worked example.
PEEK Compared With Other High-Performance Plastics
| Material | Continuous use | Chemical resistance | Wear | Cost | Notes |
|---|---|---|---|---|---|
| PEEK | Around 250 °C | Outstanding | Very good | Highest | The broadest property combination available |
| PPS | Around 220 °C | Outstanding, but not against strong oxidisers | Good | Moderate | Cheaper alternative for many chemical and electrical parts |
| PEI | Around 170 °C | Good | Moderate | Moderate to high | Transparent, good electrical performance |
| PAI | Around 260 °C | Very good | Outstanding | High | Often used for machined parts rather than moulded ones |
| PBT | Around 120 to 140 °C | Moderate | Good | Low to moderate | The workhorse for electrical housings and connectors |
| PA66 | Around 130 to 150 °C | Moderate | Good | Moderate | Widely used under-bonnet, moisture sensitive |
The comparison that saves the most money in practice is PEEK against PPS: for a large share of chemical, electrical and under-bonnet applications, PPS delivers adequate performance at a fraction of the cost. PEEK is the right answer when the temperature ceiling, hydrolysis exposure or wear duty genuinely requires it. Our comparison of PA66, PBT and PPS for automotive components is a useful reference point for where that boundary sits.
Quality and Documentation
| Requirement | What it involves |
|---|---|
| Material certificates | Batch-level certificates of analysis from the resin supplier |
| Traceability | Resin lot to production batch to shipped carton, retained for the agreed period |
| Process records | Documented melt temperature, mould temperature, cycle and hold parameters |
| Crystallinity verification | Where the application depends on it, verified by DSC or equivalent |
| Dimensional inspection | CMM or optical measurement against the drawing, after stabilisation |
| Medical documentation | Qualified processes and validated equipment for medical grades |
| Aerospace documentation | First article inspection and change control to the customer's requirements |
| Change control | Any material, tool or process change re-qualified before production |
For PEEK, the documentation matters as much as the part. A moulder who can produce a PEEK component but cannot produce a traceable process record is not supplying the industry this material belongs to.
Conclusion
PEEK is the material you specify when nothing else will survive the service conditions: continuous temperatures near 250 °C, aggressive chemistry, steam sterilisation, dry running wear, or a requirement for implantable biocompatibility. Moulding it is a different discipline from commodity work — 400 °C melt, a tool held above 175 °C with oil, hardened tooling designed for thermal expansion, and a process whose crystallinity determines whether the part performs as specified or merely looks right. The material is expensive and the process is demanding, and for the applications that need it, there is no substitute.
The most valuable engineering decision with PEEK is usually made before anyone quotes: confirming that the part really needs it, and choosing the grade — unfilled, glass filled, carbon filled or a bearing compound — that matches the actual load case. That decision, made at the design stage, typically saves more money than any negotiation on price.
With injection moulding capability from 80 to 1,400 tonnes, in-house tooling and high-temperature process equipment, we run PEEK and other high-performance polymers in unfilled, glass filled, carbon filled and bearing grades. Through our custom injection moulding services we support high-performance projects from material selection and tooling design through crystallinity control, dimensional approval and traceable volume production. Send us your part drawing and service conditions — temperature, chemical exposure, load and wear duty — to discuss grade selection and process capability for your application.
FAQ
What is PEEK injection moulding?
PEEK injection moulding is the production of parts from polyetheretherketone, a semi-crystalline high-performance thermoplastic. It is used where continuous service temperatures approach 250 °C, chemical resistance must be outstanding, or the material has to survive steam, hydrolysis and dry-running wear — applications such as aerospace components, medical instruments, semiconductor parts and chemical pump components.
What temperature does PEEK need for injection moulding?
Melt temperature is typically 380 to 400 °C, with a mould temperature of 175 to 200 °C. The high mould temperature is not optional: it drives crystallinity, and therefore the chemical resistance, dimensional stability and service temperature the part was specified for. Tooling must be oil-heated and designed to operate hot.
Does PEEK need drying before moulding?
Yes. PEEK is normally dried at 150 to 160 °C for 3 to 4 hours before processing, and kept dry up to the feed throat. Moisture produces splay, silver streaks and reduced mechanical performance — and at PEEK's material cost, discovering it after a production run is expensive.
What is the shrinkage rate of PEEK?
Unfilled PEEK shrinks about 1.0 to 1.4 percent. Glass filled and carbon filled grades shrink far less, typically 0.2 to 0.6 percent and 0.1 to 0.5 percent respectively, with strong differences between flow and cross-flow directions. Shrinkage depends heavily on mould temperature, so tooling data must come from the actual grade at the intended process conditions.
Why are PEEK parts so expensive?
For four reasons: the resin itself costs ten to twenty times commodity plastics; only high-temperature machines with corrosion-resistant screws and barrels can process it; tooling needs oil heating, hardened steels and thermal expansion design; and the narrow process window produces higher scrap rates. The material and the process are both premium, which is why PEEK is specified only where the service conditions require it.
Can PEEK be replaced by a cheaper material?
Sometimes. PPS is the most common substitute, offering outstanding chemical resistance and roughly 220 °C continuous service at a fraction of the cost, which covers a large share of chemical, electrical and under-bonnet applications. PEI and filled PBT are also options. The decision depends on the specific temperature ceiling, chemical exposure and wear duty — and is best made at the design stage rather than after tooling is cut.